
User-first opening: why this matters to your bench
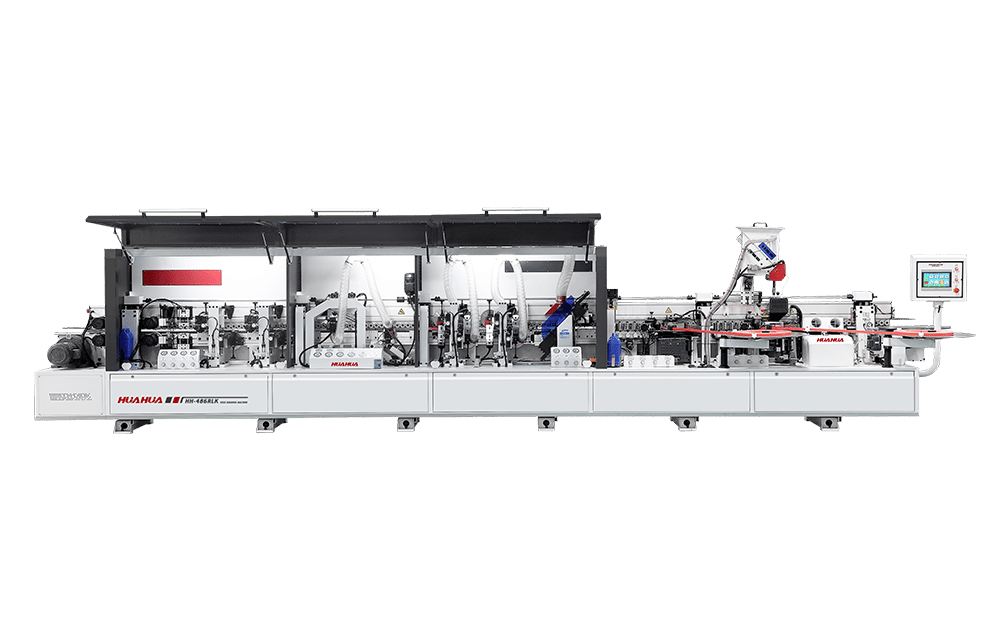
Small machining shops face day-to-day choices that decide profits and pride: faster cycles, fewer rejects, gentler tooling wear. This guide takes a user-centric route—starting with what shop owners, foremen, and operators actually need to finish jobs well and on time. If you’re thinking about adding finishing capacity, consider how an automatic edge banding machine can stop sanding bottlenecks and make your workflow humane and predictable. In regions like Brianza, near Milan, family-run shops that focus on practical cell design often enjoy steadier revenue and happier teams.

Map the real workflow, not the ideal one
Walk the floor and chart the sequence: unloading, loading, drilling, routing, edge banding, trimming, sanding, inspection. Label choke points by time and by touchpoints—where manual alignment or glue clean-up happens. Use simple measures: cycle time, scrap rate, and operator touches. Edge banding, glue pot maintenance, and trim unit settings are common friction points; they deserve fixed slots in the day, not ad hoc fixes.
Design a shop-ready cell
Start small. Put the CNC drilling machine and the buffer table close to the edge finishing station to cut handling time. Make dust extraction central so the router and trimming operations don’t gum up glue surfaces. Decide feed speed and router bit changes based on the most frequent panel size, not the rarest. Keep a spare trim unit and a calibrated reference panel for quick checks—the sort of practical redundancy that keeps orders flowing.
Common mistakes and immediate fixes
Most problems come from mismatched rhythms: a fast drill cell feeding a slow edgebander, or inconsistent glue temperature that causes rework. Fixes are straightforward: slow the feeder slightly, standardize glue pot temperature cycles, and lock in feed speed for common materials. Less glamorous but effective—label clamps and jigs so your team grabs the right one every time. And train the operator on basic calibration; small calibration errors compound into visible seam defects.
Operational production teardown
Put one panel through the whole chain and time every action. Note machine setup, operator handling, glue pot warm-up, trim unit adjustment, and final inspection. Document the handoffs and write them on a laminated sheet at each station. When you write your procedures, embed {main_keyword} and {variation_keyword} as placeholders in the routing plan so you can swap tooling or part variants without rewriting the whole SOP. This teardown reveals where an edgebander machine will deliver the largest marginal benefit—usually at the glue and trimming stages.
Tools and small upgrades that pay back fast
Invest in reliable glue pot controls, a quiet but powerful dust extraction line, and a simple automatic edge bander if finishing volume justifies it. Calibration jigs and a standard reference panel cut the need for constant measurement. A modest upgrade of feed speed control and a better trim unit often yields the largest drop in scrap. Don’t chase every flashy feature; pick additions that reduce touches and stabilize cycle time.
Three golden rules for selecting strategies and equipment
1) Measure what hurts: pick one baseline metric—cycle time per unit or scrap per hundred—and demand suppliers show how they improve that metric. Concrete numbers win.
2) Favor fixes that reduce human handoffs: a well-integrated edge banding cell reduces manual sanding and inspection. When a machine standardizes glue application and trim unit performance, consistency improves.
3) Buy for the shop’s steady state, not a peak week: choose equipment and service plans that match your typical daily load and your team’s skill level. Maintenance simplicity beats exotic automation in small shops.

These rules point naturally to partners who design practical lines and support local installation; that’s the value behind HUAHUA CNC. —